Search

Batch Anodizing Project for Small CNC Machined Parts — Case Study

Small CNC parts Anodized Project Overview

Project InfoProject Results
Client: A precision equipment components manufacturer✅ Surface integrity pass rate: 100%
Project: Batch anodizing of small aluminum CNC parts✅ Contact point concealment pass rate: 100%
Volume: 1,000 pcs per batch, max part size 20mm✅ On-time delivery rate: 100% (15 days)
Material: 6061-T6 Aluminum✅ Customer satisfaction: 5/5 stars
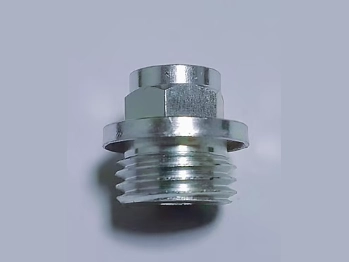
Small CNC machined aluminum fitting, 20mm size, before anodizing treatment

Client Challenge

  • Parts too small for standard fixturing. The client’s parts typically measure 15–20mm, making them too small to be individually mounted on conventional anodizing racks. Standard anodizing requires each part to be secured on a conductive fixture, which is impractical at this scale — manual handling costs and processing time quickly become unmanageable.
  • Contact-point placement was highly sensitive. A previous supplier addressed the fixturing problem by drilling holes and threading wire through the parts in bulk — leaving visible contact marks where the base metal showed through unanodized. Since these were cosmetic, exposed-surface parts, visible contact marks were an unacceptable defect for the client.
  • Batch consistency was hard to guarantee. Bulk-loading small parts together often causes uneven current distribution between parts in contact with one another, resulting in color variation or inconsistent oxide layer thickness within the same batch. The client’s previous defect rate for this issue was close to 15%.
  • Small batch size, high order frequency. Because individual part volume was so small, the client placed frequent but relatively small orders. Many anodizing suppliers either declined the work as “not worth it” or forced the client to wait and consolidate orders to reach a minimum batch size.

03 / Our Solution

Equipment Setup
Custom-designed racking/barrel fixtures specifically built for small-part anodizing.
Coating thickness gauge + batch sampling inspection system to monitor oxide layer consistency across every batch.
Process Optimization
Contact Point Planning
At project kickoff, we worked with the client to identify non-cosmetic, non-functional surfaces on each part. All conductive contact points were deliberately positioned on these concealed surfaces, eliminating visible contact marks on cosmetic faces from the design stage onward.
Custom Loading Fixtures
We designed dedicated racking fixtures matched to the part geometry, replacing the crude drill-and-wire approach. This solved both the fixturing problem for undersized parts and gave us precise, repeatable control over contact point placement across every batch.
Current Density Control
Current parameters were adjusted by zone based on part density and distribution within the tank, preventing the uneven current flow that occurs when small parts are loaded closely together — the root cause of thickness and color inconsistency.
Dedicated Scheduling
We established a dedicated production slot for this client's ordering pattern, eliminating the delays caused by waiting to "batch up" to a minimum order quantity.

This anodizing case is one example of the surface treatment challenges we solve routinely — see our full surface finishing solutions for the range of processes we offer, including black oxide, plating, and powder coating for parts that don’t fit standard processing conditions.
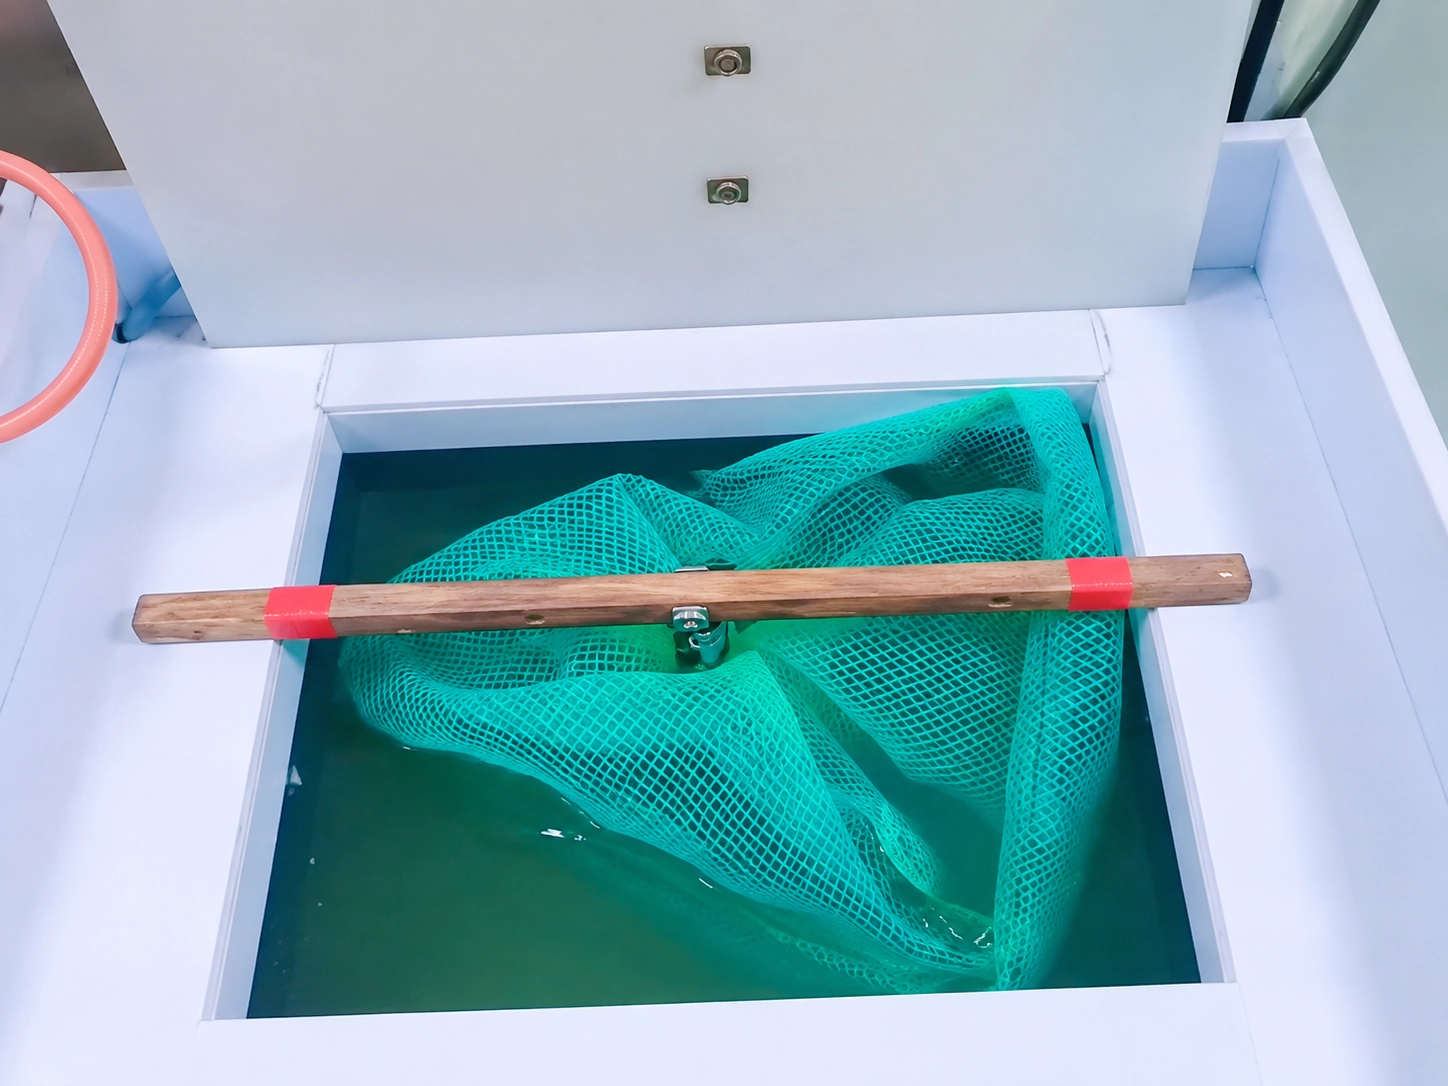
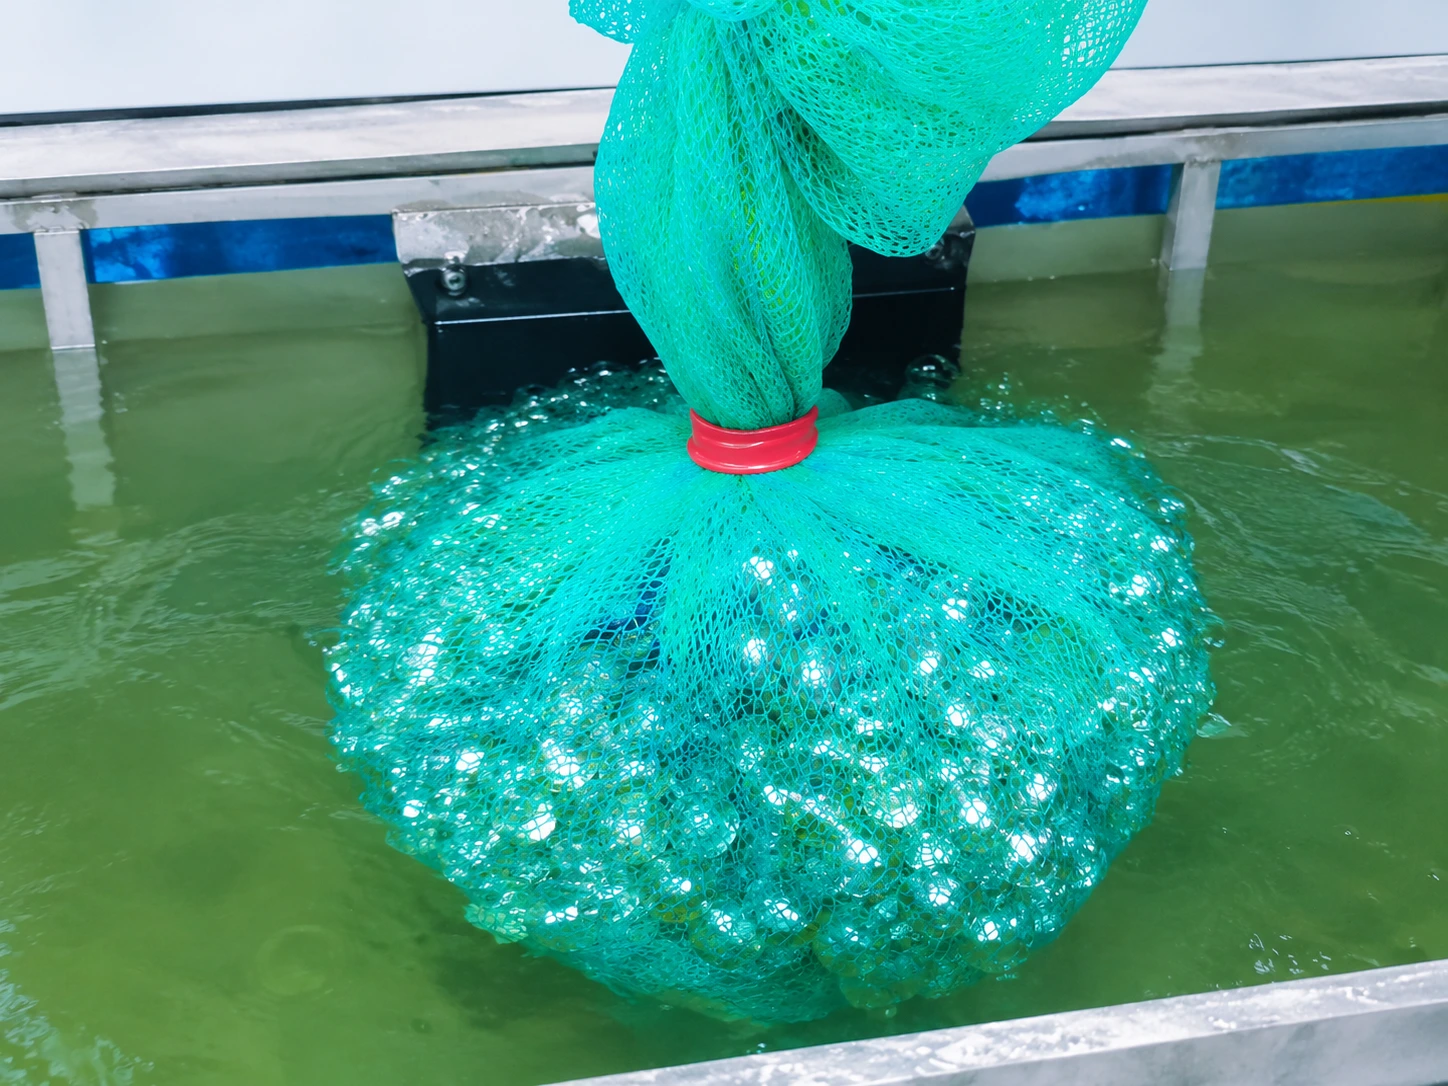
Mesh net bag batch loading method for small parts anodizing tank, replacing individual fixturing
Close-up of mesh bag containing small aluminum parts submerged in anodizing bath solution

Project Results


MetricBefore (Previous Supplier)After (Chiheng Solution)Improvement
Visible contact-mark defect rate~12% (clearly visible marks)0% (contact points on concealed surfaces)100% reduction
Batch color/thickness inconsistency rate~15%2%~86.7% reduction
Processing lead time (1,000-pc batch)20 days (waiting to consolidate volume)15 days25% faster
Minimum order quantity required5,000 pcs minimumNo minimum order requirement

Client Testimonial

“Our parts are so small that most suppliers wouldn’t even take the fixturing problem seriously — they’d just drill holes and wire them together, and the scarring was never acceptable to our customers. Chiheng worked with us before the first sample run to figure out exactly where the contact points should go. That level of attention to detail is why we made them our long-term partner.”
— Jason, Component Engineering Lead, Precision Equipment Manufacturer

Struggling with small parts that can't be individually fixtured for anodizing?

If your parts require a different surface treatment altogether — for example, corrosion protection on steel components — our black oxide finishing service addresses similar small-part handling challenges for carbon steel, alloy steel, and select stainless grades.

Custom Your Parts Now!

Stop thinking more, fill out the blank below, and send us an inquiry, and you will have a professional team of board game custom products contact you to answer any questions and provide pricing.

Get a Fast Quote

You can send us any questions to get any information you would like to know, and we will respond to you in extremely short time.

Menu

Update cookies preferences